
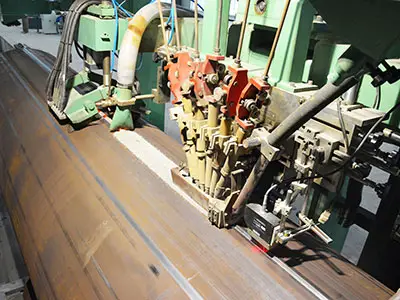
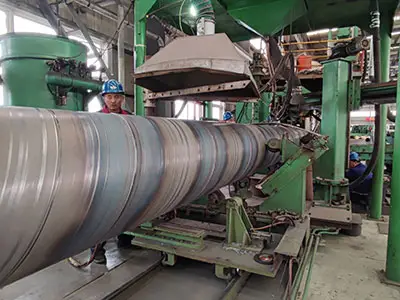
Submerged arc welding welding zone prone to defects such as porosity, hot cracks, and biting edge.
Gas bubbles. Bubbles mostly occur in the center of the weld channel, the main reason is that hydrogen is still in the form of bubbles hidden inside the weld metal, so the measures to eliminate this defect is that first of all, you must remove the wire and weld rust, oil, water and moisture and other substances, and second is that you must dry the flux very well to remove moisture. In addition, increase the current, reduce the welding speed, slow down the solidification of the molten metal is also very effective.
Sulfur cracking (sulfur-induced cracking). Cracks caused by sulfide in the sulfur precipitation zone entering the weld metal when welding plates with strong sulfur precipitation zones (especially soft-boiling steels). The reason for this is the presence of iron sulfide with a low melting point in the sulfur segregation zone and the presence of hydrogen in the steel. Therefore, in order to prevent this situation, the use of semi-sedated steel or sedated steel containing less sulfur segregation zone is also effective. Secondly, cleaning and drying of the weld surface and flux are also necessary.
Thermal cracking. In submerged arc welding, thermal cracks can be produced in the weld channel, especially in the arc starting and arc quenching arc pits are prone to cracking. In order to eliminate such cracks, usually in the arc and arc quenching equipped with pads, and at the end of the plate coil pair welding, can be reversed spiral welded pipe and will be welded into the stack welding. Thermal cracking in the weld stress is very large, or weld metal within the si is very high when the most likely to produce.
Involvement of weld slag. Involvement of weld slag is a portion of weld slag remaining in the weld metal.
Poor weld penetration. The internal and external weld metal do not overlap enough and are sometimes not welded through. This is called inadequate weld penetration.
Edge biting. Edge biting is a V-shaped groove along the centerline of the weld at the edge of the weld. Edge biting occurs when conditions such as welding speed, current, and voltage are not appropriate. Among them, too high welding speed is more likely to cause edge clenching defects than unsuitable current. Pipe distribution in the same area, and higher than the general submerged arc straight seam welded pipe.


 English