
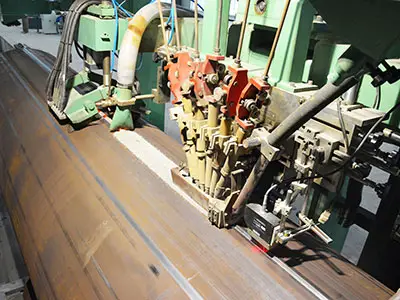
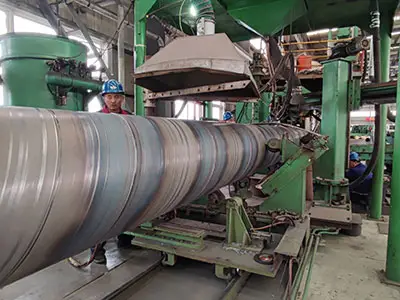
SSAW steel pipe (Spiral Submerged Arc Welded pipe) is widely used in water transmission, piling, and structural applications due to its cost-effectiveness and ability to produce large diameters. However, the spiral welding process can introduce specific welding defects that affect pipe integrity.
This article explores the most common weld defects in SSAW steel pipe, their causes, and preventive measures to ensure high-quality production.
Defect: Small cavities or bubbles within the weld metal, often along the weld centerline.
Causes:
· Hydrogen trapped in the weld due to moisture in flux, rust, or oil contamination on the steel surface.
· Insufficient pre-weld cleaning.
Prevention:
✔ Dry the flux properly before welding.
✔ Clean the steel coil edges thoroughly (remove rust, oil, and moisture).
✔ Optimize welding current and reduce speed to allow gas escape.
Defect: Cracks appearing in the weld bead, especially at the start/stop points of the spiral weld.
Causes:
· High residual stress during cooling.
· Excessive sulfur (S) content in the steel, leading to brittle zones.
· Improper welding parameters (high heat input, fast cooling).
Prevention:
✔ Use low-sulfur steel grades (killed or semi-killed steel).
✔ Implement run-on/run-off tabs to prevent crater cracks.
✔ Control interpass temperature to reduce stress buildup.
Defect: Entrapped flux residues within the weld metal.
Causes:
· Improper flux removal between weld passes.
· Incorrect welding angle in spiral welding.
Prevention:
✔ Ensure proper flux cleaning between weld layers.
✔ Adjust welding torch angle for better slag detachment.
Defect: Insufficient melting between weld metal and base material, leading to weak joints.
Causes:
· Low welding current or excessive speed.
· Misalignment in spiral seam formation.
Prevention:
✔ Optimize welding parameters (higher current, slower speed).
✔ Ensure precise edge preparation before welding.
Defect: A V-shaped groove along the weld toe, weakening the joint.
Causes:
· Excessive welding speed (most common cause).
· Incorrect voltage/current settings.
Prevention:
✔ Reduce travel speed to allow proper filler metal deposition.
✔ Adjust voltage and wire feed rate for smoother bead profile.
To minimize welding defects, manufacturers should:
✅ Conduct pre-weld inspections (material cleanliness, joint alignment).
✅ Use automated ultrasonic testing (UT) for defect detection.
✅ Follow API 5L/ISO 3183 standards for spiral weld integrity.
SSAW steel pipe offers economic advantages for large-diameter applications, but welding defects like porosity, cracks, and lack of penetration can compromise performance. By optimizing welding parameters, material selection, and quality control, manufacturers can produce high-integrity spiral welded pipes for demanding applications.
Need reliable SSAW steel pipe suppliers? Our SSAW steel pipes are manufactured under strict welding defect prevention protocols to ensure superior quality. Contact us today for your project requirements!


 English