
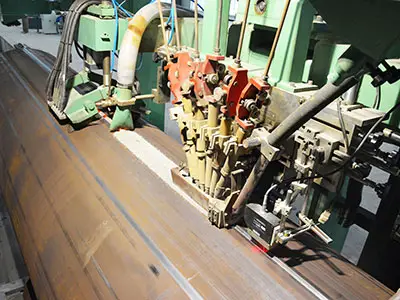
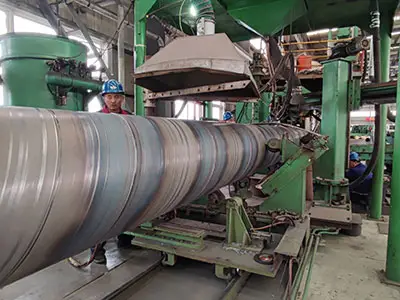
Welded steel pipe slag is residual inside the weld slag. Theoretically analyzed, submerged arc automatic welding weld slag produced by the following three main reasons: ① raw materials (including base metal, wire, flux) inclusions more; ② multi-layer welding layer cleaning is not clean; ③ selection of welding process parameters are not appropriate, is not conducive to the emergence of slag.
According to the production characteristics of LSAW steel pipe, can be excluded when the multi-layer welding layer cleaning is not clean and make the weld slag this reason. For more inclusions in the raw material to make the weld slag, take pre-welding inspection of base material, new wire and flux and other measures, the weld fusion line slag produced by the proportion of only a slight decrease in the raw material inclusions is not the main cause of slag. Therefore, thick-walled straight seam submerged arc welded steel pipe fusion line slag is the main reason for the choice of welding process parameters are not appropriate. Thick-walled straight seam submerged arc welded pipe welding process parameters are: line energy, welding current, welding voltage, welding speed, wire spacing, bevel size and so on. Then from the welding metallurgy to do an in-depth analysis can be seen: the weld fusion line slag slag is mainly due to the fusion line temperature is too low, so that the liquid slag can not be precipitated in time; and lead to the fusion line temperature is too low because of the peak temperature of the heating is too low or the cooling rate is too fast.
Cutting straight seam steel pipe is the longest method is gas cutting, gas cutting is the use of oxygen and acetylene combustion heat generated by the metal being cut at high temperature melting iron oxide slag, and then use high-pressure oxygen gas flow will be blown away from the metal at this time the straight seam steel pipe is cut off.
Cut off the straight seam steel pipe with gas cutting high efficiency, easy to operate the cut section is also relatively neat, but the surface of the cut will be attached to a layer of oxidized film. Need to remove before welding. In the straight seam steel pipe pipe installation process commonly used gas cutting method to cut a variety of larger diameter straight seam steel pipe, steel, profiles. Cutting straight seam steel pipe gas cutting tools for the torch according to the different acetylene pressure is divided into shot suction and isobaric two kinds, we commonly used is shot suction torch. Oxygen for gas cutting is supplied by oxygen cylinder, and acetylene gas is supplied by acetylene cylinder or acetylene generator.
Because of the dangers of gas cutting, it is necessary to strictly implement the operating procedures when operating with gas cutting method of cutting straight seam steel pipe should also pay attention to the following points: 1. Whether the straight seam steel pipe rotation or fixed cutting nozzle should be kept perpendicular to the surface of the straight seam steel pipe to be cut through the cutting nozzle gradually tilted to the cutting point of the tangent line tilted to the cut point at an angle of 70 ° -80 °. 2. When gas cutting and fixing the straight seam steel pipe, generally start from the lower part of the straight seam steel pipe first. 3. The selection of cutting nozzle and oxygen pressure size is related to the thickness of the straight seam steel pipe, which can be selected according to the actual situation. 4. The distance between the cutting nozzle and the surface of the LSAW pipe should be determined according to the length of the preheated flame and the thickness of the LSAW pipe, and the distance between the center of the flame and the surface of the LSAW pipe should be 3-5mm. 5. After the straight seam steel pipe is cut, the iron oxide residue at the mouth should be cut with a file or hand wheel to make it smooth and clean, and at the same time, the end surface of the straight seam steel pipe mouth should be kept perpendicular to the centerline of the pipe. 6. The end of gas cutting should quickly close the cutting oxygen valve, acetylene valve preheating oxygen valve.


 English